The 2026 market for an Autobody CNC Router is shaped by vehicle complexity, repair demand, and tighter production expectations. S&P Global Mobility reported that the average age of vehicles in the United States reached about 12.6 years in 2024. Older vehicles create steady demand for replacement panels, repair fixtures, templates, and restoration components. At the same time, the International Energy Agency reported more than 17 million electric cars sold globally in 2024. Newer vehicles often combine aluminum, composites, high-strength steel, and complex aerodynamic forms.
That material shift changes router selection. A three-axis CNC router suits flat panels, trim patterns, foam models, and basic fixtures. Four-axis equipment adds controlled rotary cutting for tubes and curved components. Five-axis systems provide better access to sculpted body surfaces and reduce manual repositioning. Automatic tool changers, vacuum tables, dust extraction, and closed-loop control can improve repeatability. The right combination depends on material thickness, panel size, tolerances, production volume, and available operator skills.
Industry reports from Grand View Research and MarketsandMarkets indicate continued growth in CNC equipment and automotive manufacturing automation. However, market forecasts are not purchasing instructions. They may not reflect local electricity standards, service coverage, or real cutting conditions. This is where many buyers hesitate, reasonably. A machine advertised for carbon fiber may perform poorly without suitable tooling and extraction. A large working bed may also waste floor space and energy. This guide compares leading Autobody CNC Router types for global buyers, focusing on practical capacity, safety, maintenance, supplier support, and measurable return on investment. No single router wins every workshop. That conclusion deserves careful review.
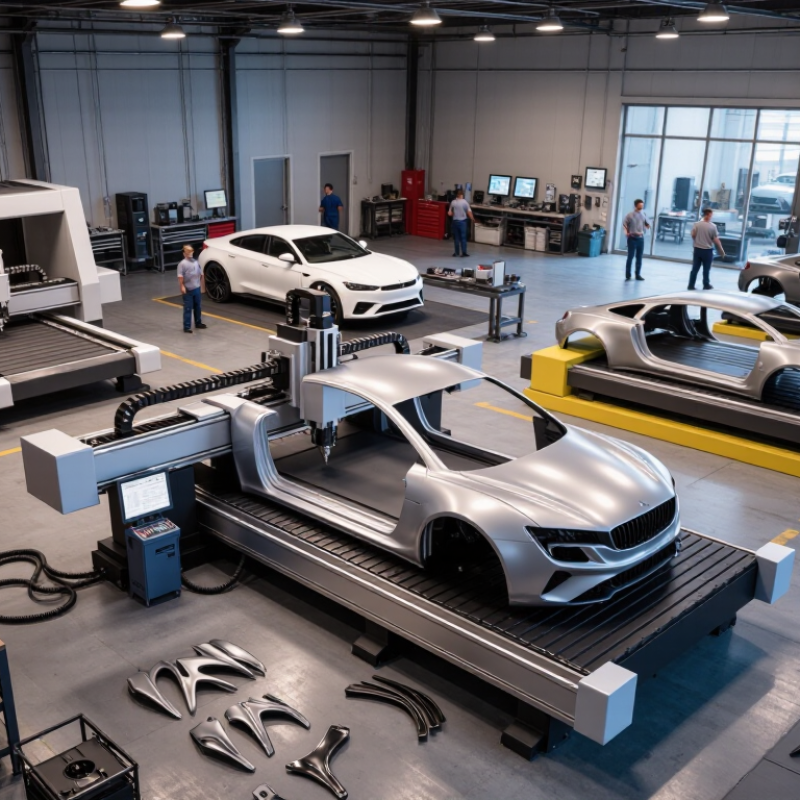
An autobody CNC router is a computer-controlled cutting system for shaping plastic, foam, composite sheets, and selected lightweight panels. It follows digital CAD drawings instead of hand-marked templates. The operator loads the material, sets the origin, chooses the tool, and checks the cutting path. Then the spindle removes material along programmed X, Y, and Z movements.
It is more controlled than manual trimming. Still, it is not magic. A 3-axis router suits flat brackets, door-card templates, and bumper patterns. A 5-axis machine handles deeper curves and angled surfaces with fewer repositioning steps. Vacuum tables hold large sheets firmly, while dust extraction protects the cutting area and improves edge quality. Tool selection matters. A blunt cutter can melt plastic or leave a rough edge.
S&P Global Mobility reported that the average U.S. vehicle age reached about 12.6 years in 2024, supporting continued repair demand. Grand View Research also identifies automation and computer-aided manufacturing as major CNC market growth drivers. These figures do not guarantee profit. Material thickness, software skill, ventilation, and operator training still decide daily results. A small alignment error can spoil an expensive panel. That part is easy to underestimate. A reliable workflow includes dry runs, measured test cuts, emergency stops, and regular spindle inspection. Safety requirements must also follow local workplace regulations.
An autobody CNC router is a computer-controlled cutting machine used to produce automotive patterns, templates, composite panels, plastic trim, foam models, and other non-metal or lightweight bodywork components. The router follows CAD/CAM toolpaths to control spindle movement along the X, Y, and Z axes. Five-axis systems can also tilt and rotate the cutting tool for more complex curved parts.
The chart compares representative maximum sheet-length formats commonly associated with different router configurations. The dimensions are shown in millimeters and reflect widely used 5-foot, 8-foot, 10-foot, and 12-foot material formats.
Autobody work needs more than cutting speed. The material, panel size, and required finish should guide router selection. A 3-axis CNC router suits flat aluminum templates, plastic panels, foam bucks, and simple replacement patterns. It is easier to program and usually costs less. However, it cannot match compound curves without extra manual shaping. That limitation matters.
A 4-axis router adds rotary movement for tubes, rails, and curved trim components. It can reduce repositioning and improve alignment around wheel arches. For full-size composite molds or large aluminum sheets, a 5-axis router offers better access to angled surfaces. It also reduces secondary cutting, though programming becomes demanding. Shop-floor experience shows that poor fixturing can still ruin an accurate toolpath. The machine is not always the weak point.
The U.S. Department of Energy reports that reducing vehicle weight by 10% can improve fuel economy by roughly 6–8%. This supports precise routing of lightweight aluminum, composites, and engineered plastics. Dust extraction is essential for composite work, while coolant control helps during aluminum cutting. A 2024 global CNC machinery market assessment valued the sector at tens of billions of dollars, reflecting strong industrial adoption. Yet market growth does not guarantee the right purchase. Buyers should test their actual panel thickness, curve radius, tolerance, and daily workload before choosing a router type. Some workshops still overbuy five-axis equipment for mostly flat parts. That choice deserves reconsideration.
Comparing an autobody CNC router starts with the material, not the advertised spindle speed. Plastic bumpers, aluminum sheets, composite panels, and foam patterns require different cutting behavior. A 3.0 kW spindle may suit trim parts and templates, while thicker composite work can need higher torque and better cooling. Grand View Research reported that the global CNC machine market reached about USD 88.9 billion in 2023, with continued growth expected through 2030. That expansion does not mean every machine fits autobody work.
Check the working table carefully. A 1,300 × 2,500 mm bed can handle many vehicle panels, but door skins may still require repositioning. Repeated repositioning can reduce accuracy. Look for stated positioning accuracy, repeatability, vacuum-zone design, and gantry rigidity. Dust extraction also matters, especially when cutting fiberglass or carbon-based composites. The International Energy Agency’s 2024 energy-efficiency analysis highlights rising industrial attention to efficient motor systems, so compare spindle power with actual energy consumption.
Software compatibility deserves equal attention. Test whether the controller accepts common CAD/CAM files and supports toolpath simulation. Ask for sample cuts using your own panel thickness. I would not trust a brochure’s accuracy claim without a physical test. It sounds obvious, but it is often missed. Global buyers should also verify voltage, emergency-stop design, guarding, training, spare-part access, and local service response. MarketsandMarkets has identified automation and connected monitoring as major manufacturing trends, yet basic maintenance remains decisive. Fancy monitoring cannot repair a poorly aligned gantry.
Autobody CNC routers handle more than replacement panels. They commonly cut aluminum sheet, ABS, HDPE, acrylic, PVC, polyurethane foam, and fiberglass composites. Carbon-fiber panels are also possible, but they demand sharp tooling, strong dust extraction, and controlled feeds. Hardened steel is usually unsuitable for standard router systems. It needs industrial milling equipment instead.
The IEA Global EV Outlook 2024 recorded more than 17 million electric-car sales worldwide in 2024. That growth increases demand for lightweight aluminum, plastic, and composite components. Aluminum cuts cleanly when the machine uses proper chip clearance and lubrication. ABS and HDPE produce curled chips and may melt under excessive spindle heat. Foam cuts easily, but thin sections can deform during clamping.
Composite work is less forgiving. Fiberglass dust can irritate skin and lungs, while carbon-fiber dust may damage electrical parts. A sealed vacuum table helps, but it is not a complete safety solution. The U.S. National Institute for Occupational Safety and Health recommends effective local exhaust ventilation for airborne machining contaminants. Real workshops still see poor results when operators ignore fixturing or tool wear. That part needs honest attention. Material charts are useful, yet actual results vary with thickness, resin content, cutter geometry, and machine rigidity.
2026 Top Autobody CNC Router Types for Global Buyers
Global buyers should match the router type to real autobody work, not catalogue pictures. A three-axis router suits plastic panels, foam forms, trim boards, and cutting templates. A four-axis model offers better access around curved components. Check the working area against your largest panel, leaving room for clamps and safe movement. Spindle power matters, but excessive power can damage thin materials. Ask for cutting samples before purchase.
Installation needs practical planning. Place the machine on a rigid, level floor with enough clearance for loading sheets. Confirm local voltage, grounding, ventilation, and dust extraction requirements. A qualified technician should check cable routing and emergency-stop function. Calibrate the X, Y, and Z axes with a test grid. Small alignment errors can create visible panel gaps. I have seen buyers blame software when the real problem was an uneven floor.
Tips: Keep the workshop clean. Remove dust from rails after each shift. Inspect belts, collets, cutters, and vacuum lines weekly. Record unusual vibration or cutting noise early. Replace worn tools instead of forcing them through material. Maintenance schedules are useful, but they are not perfect; humidity, dust, and operator habits change wear rates. Review the schedule after the first month, then adjust it using measured service records. Keep spare consumables available, but avoid storing them in damp areas.
Comparative guide to common CNC router configurations used for automotive body panels, composite components, interior parts, molds, templates, and repair-shop fabrication.
| CNC Router Type | Typical Working Area | Typical Spindle Range | Typical Accuracy | Best-Fit Autobody Applications | Main Selection Advantage | Installation Priorities | Routine Maintenance | Main Limitations |
|---|---|---|---|---|---|---|---|---|
| 3-Axis Gantry Router | 1,300 × 2,500 to 2,100 × 3,100 mm; Z-axis travel commonly 200–300 mm | 3–9 kW; approximately 12,000–24,000 rpm | Approximately ±0.05–0.15 mm, depending on machine construction and calibration | Flat composite panels, plastic sheets, foam patterns, plywood templates, aluminum trim, and non-structural body components | Simple programming, broad tooling compatibility, and lower initial complexity | Level concrete floor, stable anchoring, dust extraction, electrical grounding, and sufficient clearance around the gantry | Clean linear guides and rack-and-pinion drives; inspect belts, bearings, collets, cables, and sacrificial bed; verify squareness regularly | Cannot machine undercuts or complex angled surfaces without repositioning the workpiece |
| 4-Axis Router with Rotary Attachment | Flat-bed area commonly 1,300 × 2,500 mm; rotary diameter approximately 200–400 mm | 4–9 kW; approximately 12,000–24,000 rpm | Approximately ±0.08–0.20 mm; rotary accuracy depends on indexing and chuck alignment | Tube-like parts, wheel forms, column trims, buck sections, cylindrical patterns, and parts requiring indexed side machining | Adds indexed rotary machining while retaining many 3-axis functions | Provide a rigid rotary mounting area, align the rotary axis with the machine coordinates, and reserve space for longer workpieces | Check chuck or fixture runout, lubricate rotary bearings as specified, inspect drive backlash, and recalibrate the rotary axis after relocation | Less suitable than a true 5-axis system for continuous compound surfaces and simultaneous multi-angle cutting |
| 5-Axis CNC Router | Approximately 1,500 × 3,000 mm; Z-axis travel often 500–800 mm | 9–15 kW; approximately 12,000–24,000 rpm | Approximately ±0.05–0.12 mm when properly calibrated and fixtured | Complex composite body panels, molds, aerodynamic parts, deep cavities, sculpted interiors, and multi-sided prototypes | Machines multiple faces and steep angles in fewer setups, reducing manual repositioning | Requires a rigid foundation, accurate tool-center-point calibration, advanced CAM software, trained operators, and generous safety clearance | Check rotary-axis calibration, inspect spindle bearings and tool holders, clean motion components, back up parameters, and verify collision limits | Higher purchase, training, programming, and maintenance costs; unnecessary for simple flat-sheet work |
| ATC Nesting Router | Commonly 2,100 × 3,100 mm or 2,100 × 4,100 mm; Z-axis travel around 200–300 mm | 6–12 kW; approximately 12,000–24,000 rpm | Approximately ±0.05–0.15 mm, subject to vacuum-table condition and material stability | High-volume cutting of panels, door inserts, interior boards, templates, gaskets, and mixed-material production kits | Automatic tool changes reduce setup time and support repeated production with several cutters | Install a correctly sized vacuum system, provide clean compressed air if required, reserve tool-change clearance, and configure dust collection | Clean and inspect vacuum zones, seals, tool holders, sensors, automatic tool changer fingers, filters, and dust-collection ducts | Higher utility consumption and more components to service; vacuum performance drops when the table or seals are contaminated |
| Compact CNC Router | Approximately 600 × 900 to 1,300 × 2,500 mm; Z-axis travel commonly 80–200 mm | 1.5–4.5 kW; approximately 12,000–24,000 rpm | Approximately ±0.10–0.25 mm, depending on frame stiffness and workholding | Small repair parts, trim samples, foam models, plastic panels, signage templates, and low-volume prototyping | Lower space requirement, simpler installation, and easier entry for small workshops | Use a rigid bench or compact stand, verify electrical compatibility, provide local extraction, and secure the workpiece firmly | Remove chips after each job, lubricate linear motion parts, inspect fasteners and collets, and check frame vibration or movement | Limited cutting envelope, lower rigidity, and reduced productivity for large or thick automotive components |
It can process aluminum, ABS, HDPE, acrylic, PVC, polyurethane foam, and fiberglass composites. Carbon-fiber panels are also possible. Hardened steel usually requires industrial milling equipment instead.
Yes, aluminum cuts cleanly with suitable tooling, chip clearance, and lubrication. Poor settings can leave rough edges or heat marks. Test a small section first.
ABS and HDPE create curled chips and may melt under excessive spindle heat. Lower cutting heat and proper chip removal improve results. The same settings may not suit both plastics.
Yes, polyurethane foam cuts easily with suitable cutters. Thin sections may deform during clamping. Use gentle, even support.
Fiberglass dust can irritate skin and lungs. Carbon-fiber dust may damage electrical parts. Use local exhaust ventilation and enclosed dust collection where practical.
A three-axis router suits plastic panels, foam forms, trim boards, and templates. A four-axis model offers better access around curved components. Match the working area to your largest panel.
Confirm floor rigidity, leveling, local voltage, grounding, ventilation, and dust extraction. Leave clearance for sheet loading and clamps. Check emergency-stop operation carefully.
Calibrate the X, Y, and Z axes with a test grid. Clean dust from rails after each shift. Inspect belts, collets, cutters, and vacuum lines weekly.
Review the schedule after the first month using actual service records. Humidity, dust, and operator habits change tool wear. Published schedules are only starting points.
This guide explains how an Autobody CNC Router uses computer-controlled movement, cutting tools, and programmed designs to process automotive materials with speed and accuracy. It reviews different router types for applications such as body panel shaping, interior component production, mold making, trimming, engraving, and prototype development. Readers will learn how to match machine structure, working area, spindle power, motion accuracy, software compatibility, dust collection, and safety functions with their specific production requirements.
The article also covers materials commonly processed by an Autobody CNC Router, including plastics, composite boards, foams, wood-based panels, aluminum sheets, and other suitable non-ferrous materials. For global buyers, it provides practical guidance on comparing specifications, confirming electrical and operating requirements, planning installation space, training operators, and establishing regular maintenance routines. Careful selection and proper upkeep can improve cutting consistency, equipment lifespan, workplace safety, and overall production efficiency.