
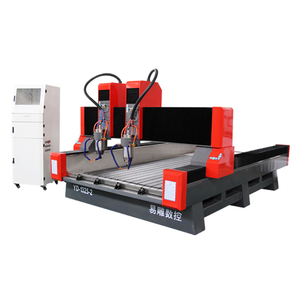
Engineered with stress-relieved steel frames, high-torque water-cooled spindles, and zero-backlash drives designed for high-density quartz, marble, and tough Nordic granites.
Why leading stone fabricators in Oslo, Larvik, Bergen, and Trondheim partner with our manufacturing facility.
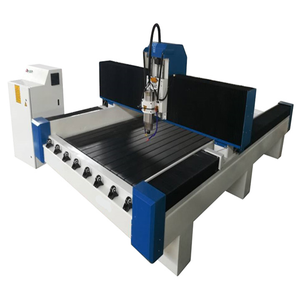
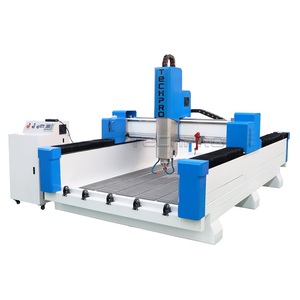
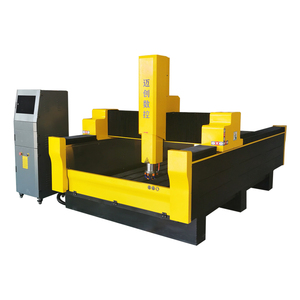
Our stone CNC routers utilize heavy-walled welded tubular steel structures that undergo annealing heat treatment at 600°C to relieve internal stresses. This guarantees zero frame deformation and dampens high-frequency resonance when machining tough Norwegian Larvikite and hard granites.
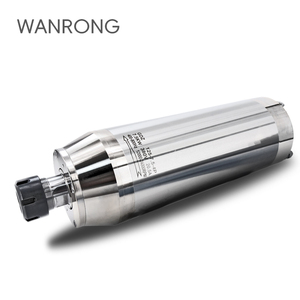
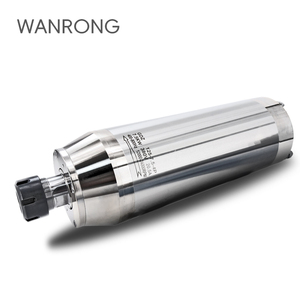
Equipped with 5.5kW to 7.5kW bullet-type spindles running on quadruplicate ceramic bearings. Operating smoothly up to 24,000 RPM, our spindles maintain full torque at lower RPM bands for deep profiling without stalling or chipping expensive slab edges.
Specially customized for Nordic climate conditions. Includes closed-loop anti-freeze thermal management options, stainless steel (SS304) water reclamation channels, and IP65 dust-and-water sealed linear guides to prevent cold-temperature slurry seizure.
Utilizing high-precision helical rack-and-pinion paired with Japanese Shimpo or German planetary gearboxes. Delivers repeat positioning accuracy of ±0.02mm across full 3x2 meter cutting beds, critical for tight-tolerance architectural stone cladding.
Powered by advanced Syntec or NcStudio controllers supporting RTCP (Rotational Tool Center Point) and 5-axis interpolation. Allows effortless 3D relief carving, beveling, column machining, and complex drainboard slope milling.
Factory configured with dual-voltage transformers capable of handling Norway’s unique IT 230V 3-phase system alongside standard TN 400V grids. Fully pre-wired with Schneider electronics and CE safety interlocks for immediate factory sign-off.
Technical Insights for Quarry Operators, Monument Crafters, and Architectural Stonemasons in Norway
Norway possesses one of the world's most unique natural stone landscapes. From the globally famous Larvikite (Blue Pearl and Emerald Pearl granite) quarried in the Vestfold region to Iddefjord Granite, Anorthosite in Rogaland, and quartz-rich slate from Oppdal and Alta, processing Nordic natural stone demands CNC machinery engineered with uncompromised rigidity and precise hydraulic cooling.
Standard CNC routers built for soft wood or light acrylic fabrics fail rapidly when introduced to the high mineral hardness of Norwegian stones. Larvikite, for example, features feldspar megacrysts exhibiting schillerization (labradorescence), which creates high shear resistance during rotary cutter engagement. Machine frames that lack sufficient damping mass experience high-frequency harmonics, resulting in tool chipping, surface micro-fracturing, and short spindle bearing life.
To assist Norwegian technical managers, plant directors, and workshop owners in evaluating equipment capability, the table below highlights the critical engineering differentials required for sustainable stone fabrication in Nordic operational environments:
| Engineering Component | Standard Commercial CNC Router | Norwegian Heavy-Duty Spec Stone Router | Operational Impact on Stone Fabrication |
|---|---|---|---|
| Bed Frame Structure | Thin-walled light steel (3-5mm) | Heavy annealed tubular steel (8-12mm), stress-relieved | Prevents frame deformation; absorbs cutting vibration during deep Larvikite slotting. |
| Spindle Type & Torque | 3.5kW Air-Cooled spindle (High RPM, Low Torque) | 5.5kW - 7.5kW Bullet Water-Cooled spindle (High Low-End Torque) | Sustains heavy diamond tool loads without thermal overload; eliminates edge micro-chipping. |
| Linear Transmission | Standard ball screw on Z, square rails without seals | Industrial sealed PMI/HIWIN linear guides + helical zero-backlash racks | Protection against abrasive stone slurry; maintains 0.02mm accuracy over years of continuous use. |
| Electrical Compliance | Standard single-voltage grid setup | Dual IT 230V / TN 400V 50Hz transformer integration | Seamless installation in Norway's unique IT grid network without tripping main breakers. |
| Slurry Management | Basic gravity drip tray | Recirculating SS304 stainless tank with multi-stage filter pump | Complies with Norwegian Arbeidstilsynet workplace silica dust and water recycling guidelines. |
A frequent failure point for imported CNC machinery in Scandinavian facilities occurs during winter shutdowns. When heating in uninsulated stone-cutting sheds is turned down overnight, residual water inside unsealed spindle jackets can freeze, causing internal cooling sleeves to rupture. Our Norwegian-bound stone routers feature closed-loop cooling circuits engineered for glycol-water mixtures, supplemented by automatic thermal purge valves that safeguard spindle assemblies against frost damage.
Furthermore, indoor air quality standards enforced by Norway’s Labour Inspection Authority (Arbeidstilsynet) mandate strict mitigation of respirable crystalline silica (RCS) dust. Our machines combine high-volume water flood nozzles (targeting the exact diamond tool contact zone) with optional full-enclosure splash guards, maintaining clean workshop environments and ensuring 100% regulatory compliance for municipal building inspectors.
From gravestone production in Viken to architectural facade fabrication in Vestland, our stone routers power diverse regional industries.
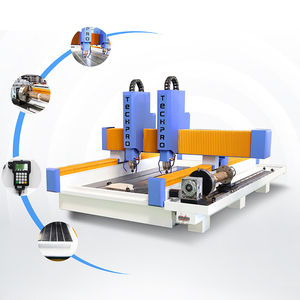
Widely utilized by Norwegian monument crafters in Viken, Innlandet, and Trøndelag. The 4-axis dual-head machines enable synchronized V-carving of traditional Norwegian lettering, intricate floral reliefs, and custom portrait engravings into black granite and polished Larvikite headstones.
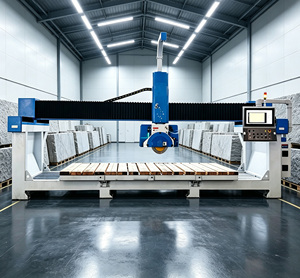
Essential equipment for stonemasons in Vestfold & Telemark processing raw blocks into polished architectural cladding panels, hotel reception desks, and custom kitchen countertops with integrated sink cutouts and precision drainboard fluting.
Utilized by historical building contractors in Bergen and Nidaros (Trondheim) for 3D laser-scanned replication of gothic soapstone carvings, decorative columns, gargoyles, and ornate church masonry requiring complex 5-axis toolpath interpolation.
Employed by civil engineering suppliers across Oslo and Rogaland to produce heavy granite street benches, bollards, public park fountains, and tactile paving stones capable of withstanding harsh Nordic winter salt exposure.
Clear, direct answers regarding power grid compatibility, shipping to Norwegian ports, maintenance, and technical support.
Yes, absolutely. Unlike most European countries that standardized exclusively on TN 400V, much of Norway’s electrical infrastructure still operates on an isolated-ground IT 230V 3-phase grid. We configure your machine's electrical cabinet at our factory with custom multi-tap isolation transformers, ensuring stable operation without neutral reference issues.
Larvikite is a high-density syenite containing large feldspar crystals that exert significant thermal and mechanical stress on router tooling. Our machines succeed here due to our heavy 12mm annealed steel frames and high-torque 7.5kW bullet spindles, which eliminate chatter and allow clean feed rates of 3,000–6,000 mm/min without edge flaking.
All machines delivered to the Norwegian market carry full CE certification under the EU Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and EMC Directive 2014/30/EU. Integrated high-volume water coolant systems comply with Arbeidstilsynet workplace regulations by completely suppressing respirable silica dust.
Ocean freight shipment from our factory directly to major Norwegian ports (Oslo, Larvik, Kristiansand, Bergen, Brevik) typically takes between 28 and 35 days. We handle export customs documentation, ISPM 15 heat-treated wooden crating, and can arrange DDP (Delivered Duty Paid) door-to-door delivery straight to your workshop floor.
Every machine comes standard with free lifetime live technical support via phone, video link, and remote control assistance. For on-site commissioning, our engineering technicians can travel to your facility in Norway to perform installation, level calibration, controller setup, and hands-on staff training in CAM programming.
Our stone CNC routers are engineered specifically for wet environments. All linear guides and ball screws feature double-lip wiper seals and automatic centralized oil lubrication pumps. Daily routine maintenance simply involves washing down the SS304 water table channels and checking pump suction filters.
Contact our application engineering team today to receive detailed technical specifications, custom machine configurations, and a competitive factory-direct quote delivered to your inbox.