
Explore high-performance 3-axis to 5-axis CNC controllers, closed-loop stepper kits, AC servo drivers, and heavy-duty slide tables engineered for high-precision OEM machinery.
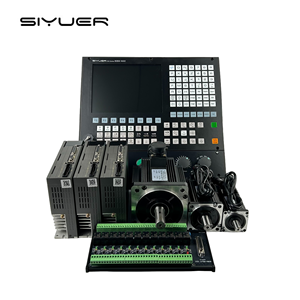
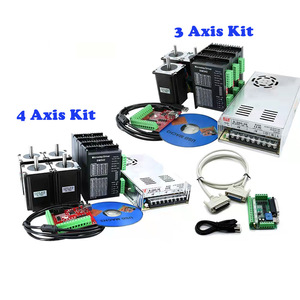
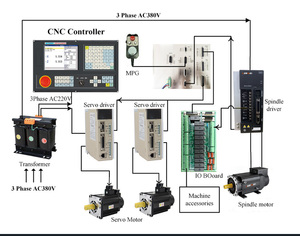
We bridge advanced motion control research with scalable manufacturing, delivering enterprise CNC controllers designed for zero-downtime industrial automation.
Our controllers incorporate open-architecture CODESYS PLC environments with real-time EtherCAT fieldbus communication, ensuring deterministic dynamic synchronization up to 32 axes.
Built for demanding shop environments with 4-layer PCB optical isolation, Class-3 EMC noise immunity, and ruggedized aluminum alloy enclosures rated for 24/7 continuous operation.
Full-scope customization available: custom front panel design, proprietary macro programming, specialized firmware logic, branded software interfaces, and expansion I/O design.
Advanced S-curve acceleration and 2000-block look-ahead processing yield continuous high-speed trajectory planning for smooth surface finishes in complex 3D VMC milling.
We deliver complete, pre-configured motion packages—including high-torque NEMA steppers, closed-loop drivers, and AC servo motors from 200W to 5kW matched to our controllers.
Backed by experienced motion control application engineers providing live remote assistance, complete wiring documentation, CAD models, and same-day global spare parts dispatch.
Modern industrial automated manufacturing requires unprecedented levels of precision, throughput, and system flexibility. As global original equipment manufacturers (OEMs) transition from conventional analog and pulse-based command interfaces to high-speed digital fieldbus systems, understanding the underlying electronics, motion algorithms, and control topology is critical for maximizing equipment longevity and competitive advantage.
Information Gain Key Takeaway: Sourcing high-efficiency CNC controllers from top Chinese manufacturing hubs allows equipment builders to reduce total BOM costs by 35% to 50% while gaining access to advanced EtherCAT fieldbus architecture and open-source PLC integration.
Historically, standard CNC control systems relied on high-frequency Pulse/Direction (P/D) signals transmitted via step-and-direction output channels to govern motor positioning. While P/D architecture remains highly effective for standard 3-axis routers and light-duty milling applications (such as NEMA23 and DM556 step-driver configurations), it introduces potential signal degradation, electrical noise interference, and wiring complexity as axis counts scale.
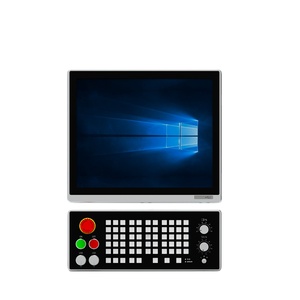
Next-generation systems—exemplified by advanced industrial panels like the Panelmate 3MK and TSINGZIWA platforms—utilize EtherCAT (Ethernet for Control Automation Technology). EtherCAT provides deterministic real-time communication with cycle times down to 100 microseconds. By replacing discrete multi-wire bundles with standard CAT5e/CAT6 shielded cables, machine builders achieve:
The core intelligence of a CNC controller lies in its motion trajectory planning module. Standard trapezoidal acceleration profiles cause instantaneous torque jerks, leading to mechanical vibration, tool wear, and visible surface chattering on machined workpieces. Advanced Chinese VMC controllers incorporate S-curve (Jerk-limited) acceleration profiling alongside multi-block look-ahead algorithms.
By evaluating up to 2,000 future G-code blocks in real-time, the control system calculates optimal cornering speeds, automatically throttling feed rates during sharp radius transitions and accelerating linearly on long vector paths. This continuous velocity management maintains constant cutter chip load, extending spindle tool life and reducing total cycle execution times by up to 28%.
To assist procurement managers and automation engineers in specifying the correct control platform, the matrix below details operational parameters across major machine categories:
| Controller Series Class | Supported Axis Range | Primary Interface Protocol | Target Machine Application | Max Pulse Output / Cycle Time | Recommended Drive Architecture |
|---|---|---|---|---|---|
| Entry-Level Compact (Mach3/USB) | 3 - 4 Axis | USB / LPT Parallel | Wood Routers, DIY Metal Engravers | 100 kHz - 200 kHz | Open-Loop Stepper (DM542/DM556) |
| Dedicated Standalone Router/Mill | 3 - 5 Axis | Pulse/Dir + Modbus RTU | Heavy Wood Carving, VMC Milling, Mold Making | 500 kHz - 1 MHz | Closed-Loop Stepper / AC Servo (200W-1kW) |
| Dedicated Plasma Controller (F2100B) | 2 - 3 Axis | Integrated Arc Voltage THC | Gantry & Tabletop Plasma Cutting | 200 kHz High Noise-Isolated | Heavy-Duty Stepper / Hybrid Servo |
| EtherCAT Industrial Panel (Codesys) | 4 - 32 Axis | EtherCAT Industrial Fieldbus | Multi-Tasking Machining Centers, Automation Lines | 100 µs Cycle Time | Absolute Encoder AC Servos (A5/A6 Series) |
Selecting the appropriate drive actuator kit is as vital as choosing the central control panel. A frequent decision point during machine engineering involves choosing between hybrid closed-loop steppers and true AC brushless servo systems:
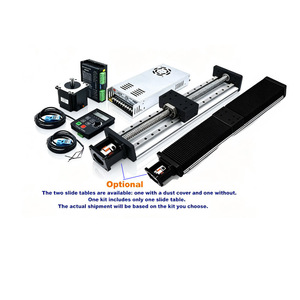
Closed-Loop Stepper Kits (e.g., NEMA23 with Optical Encoder): These systems integrate an optical encoder on the back of a high-torque stepper motor. The driver continuously monitors position lock, eliminating the risk of lost steps during heavy cut passes. Closed-loop steppers provide maximum hold-torque at low RPMs (0–600 RPM) at a fraction of the cost of AC servos, making them the optimal solution for woodworking routers, plasma cutters, and linear slide actuator tables.
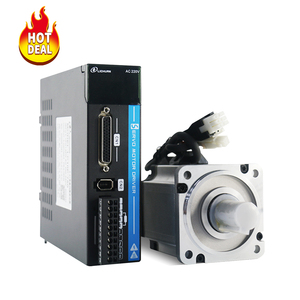
AC Servo Motor & Driver Kits (e.g., A5 200W - 1000W 220V): AC servos maintain constant torque across high operational speed bands (up to 3000+ RPM) with high dynamic response. Equipped with 17-bit or 23-bit absolute encoders, AC servos provide sub-micron positioning accuracy, making them mandatory for high-precision VMC metal milling centers, high-speed drilling machines, and industrial automatic tool-changer (ATC) platforms.
The global CNC controller market is undergoing a structural shift. Machine tool integrators across North America, Europe, and Latin America are increasingly diversifying their supply chains away from legacy high-cost proprietary systems toward agile, open-architecture control packages manufactured in specialized Chinese tech ecosystems.
Clear technical guidance for machinery importers, OEM system integrators, and plant engineers sourcing CNC control hardware.
A standalone CNC controller (such as the 808M-MAX or 990MDC) runs on an embedded real-time operating system (RTOS) hosted on industrial-grade ARM/FPGA hardware. It operates independently without requiring an external computer, eliminating crashes caused by operating system updates or background tasks. In contrast, PC-based systems like Mach3 rely on a host computer connected via USB or parallel port, making them suitable for light-duty routing and prototyping, whereas standalone panels are engineered for 24/7 industrial production environments.
Pulse/Direction controllers are cost-effective, straightforward to wire, and perfectly suited for 3-axis to 4-axis machinery using standard or closed-loop stepper drivers up to 1MHz pulse frequencies. If your equipment requires 5-axis continuous machining, rapid tool changers (ATC), absolute position feedback from AC servos, or multi-station synchronization, an EtherCAT controller provides high-speed digital communication over a single bus cable, reducing wiring complexity and boosting noise immunity.
Yes. We provide complete OEM/ODM manufacturing services for machinery manufacturers. This includes custom front membrane panel graphics, custom silkscreen logo printing, customized booted firmware splash screens, specialized macro programming for automated tool setup, and custom I/O expansion board configurations to meet your exact branding and functional requirements.
Dedicated plasma controllers monitor the electrical arc voltage between the plasma torch electrode and the metal plate during cutting operations. As the sheet metal warps due to heat or surface irregularity, the controller automatically adjusts the Z-axis torch position in real-time to maintain a constant standoff distance, preventing tip collisions and maintaining uniform cut kerf quality.
Our A5 series AC servo kits (ranging from 200W to 1000W) operate on standard single-phase or three-phase 220V AC input. They come paired with matching digital AC servo drives that convert mains power directly, eliminating the need for bulky external step-down transformers. For stepper motor configurations, standard 36V to 48V DC regulated switching power supplies (such as 350W 36V units) are typically utilized.
Yes. All of our industrial-class controllers feature non-volatile memory recording. In the event of an unexpected electrical power outage or emergency stop, the system automatically saves the exact G-code line, tool coordinates, and modal state. Once power is restored, the operator can perform a seamless one-touch breakpoint resume without scrapping valuable raw materials.
Whether you are engineering a high-speed VMC milling center, an industrial wood router, a plasma cutting gantry, or a multi-axis automation line, our technical application team is ready to assist with system specification, custom software integration, and bulk OEM pricing.