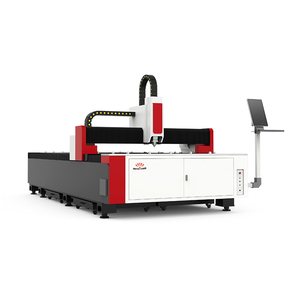
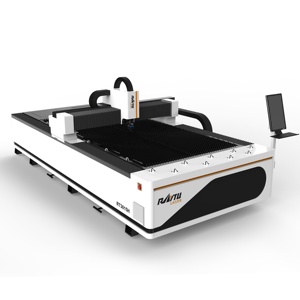
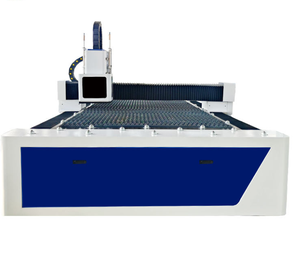
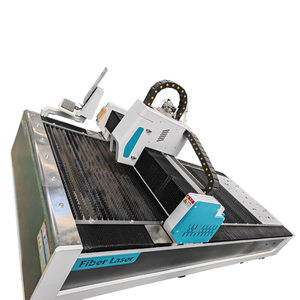
4015 Fiber CNC Laser Cutter 6000W 8000W 12000W
- Power Output: 6KW - 12KW Fiber
- Workbed Area: 4000mm x 1500mm
- Rotary Capacity: Ø20mm - Ø320mm
- Certification: CE / ISO9001 / TÜV
Industrial-grade rotary cutting, engraving, and 4th-axis machining hardware built for precision sheet metal, structural pipe processing, and automated manufacturing lines.
Understanding the kinematic precision, mechanical rigidity, and electrical compliance required for tier-1 industrial 4th-axis rotary integration.
In modern high-speed CNC milling, CO2 laser engraving, and high-power fiber laser tube-cutting applications, adding a 4th rotary axis (A/B/C rotation angle) shifts machinery performance from 2D panel processing to 3D cylindrical fabrication. However, integrating a rotary axis into industrial environments requires strict adherence to international safety, thermal, and mechanical standards—principally the European Union’s CE Marking Directives (Machinery Directive 2006/42/EC, Low Voltage Directive 2014/35/EU, and Electromagnetic Compatibility Directive 2014/30/EU).
As a leading CE Certified Rotary Axis Manufacturer & Supplier, our technical whitepaper explores the critical engineering parameters buyers and OEM system integrators must specify to prevent kinematic vibration, maintain positional accuracy across long duty cycles, and eliminate thermal growth during continuous multi-shift production.
Utilizing planetary gearboxes or strain wave (harmonic drive) speed reducers configured with zero axial play. Achieves dynamic rotational positioning under 1.5 arcminutes, crucial for seamless pipe-beveling and 3D surface engraving.
Fully compliant with EN 60204-1 electrical safety standards. Features dual-channel safety relay loops, dynamic braking, and emergency stop interlocks to safeguard technicians against unexpected rotational torque inertia.
Equipped with double-action pneumatic 3-jaw/4-jaw chucks or hydraulic clamping fixtures. Delivers self-centering accuracy within ≤ 0.01mm runout, supporting heavy structural steel pipes up to 500kg without slip.
Thermal Expansion Compensation: Standard rotary units suffer positional drift when operated continuously above 3,000 RPM due to heat build-up inside the gearhead. Our CE-certified units incorporate integrated thermal dissipation fins and optional oil-chilling jackets, ensuring zero thermal drift across 24/7 industrial operational cycles.
Strategic analysis of technological shifts shaping the next decade of multi-axis CNC machining, laser tube processing, and robotic automation.
As global manufacturing transitions toward Industry 4.0 architecture, purchasing departments are moving beyond simple price-per-watt or table-size comparisons. Procurement strategies now prioritize interoperability, dynamic payload balancing, energy efficiency, and predictive sensor monitoring. Below are the key engineering trends driving rotary axis sourcing globally:
Manual clamping introduces human error and variable clamping torque, leading to deformed thin-walled tubing or slippage of heavy solid bar stock. Modern fiber laser tube cutting systems require fully automated pneumatic chucks connected via EtherCAT or CANopen industrial fieldbus protocols. This enables real-time pressure adjustment based on tube material (e.g., lower pressure for thin aluminum, higher hydraulic force for thick carbon steel).
Traditional stepper-driven rotary axes are rapidly being phased out in high-end manufacturing. Buyers now mandate AC Servo drives (such as Yaskawa Sigma-7 or Delta ASDA series) paired with 24-bit absolute optical encoders. This eliminates the need for manual zero-point homing after power cycles and guarantees zero step-loss even during sudden high-acceleration laser vector direction changes.
To reduce cycle times in marking, engraving, and cutting, factories are deploying hybrid workstations featuring dual laser wavelengths (e.g., 1064nm Fiber combined with 450nm Blue Diode or 10.6µm CO2). The rotary axis must support dynamic multi-origin offset synchronization in software engines like CypCut or LightBurn, dynamically adapting laser focal length based on tube geometry.
Regulatory scrutiny across North America (UL/CSA standards) and the European Union (CE Mark) has made uncertified rotary components a liability for OEM equipment builders. Sourcing from certified manufacturers ensures full compliance with electromagnetic compatibility (EMC), low voltage safety (LVD), and structural safety factors, reducing import customs friction and workplace liability.

Comprehensive benchmarking of rotary axis configurations across machine classes to assist engineering teams in specifying the correct hardware configuration.
| Rotary Model / Class | Drive Architecture | Max Torque (Nm) | Backlash (Arcmin) | Runout Tolerance | Chuck Capacity | CE Certification |
|---|---|---|---|---|---|---|
| RA-Micro Desktop | Harmonic / Stepper | 12 Nm | < 2.0 Arcmin | ≤ 0.015 mm | Ø10mm - Ø80mm | ✓ Certified CE |
| RA-Standard CO2/Fiber | Planetary / AC Servo | 45 Nm | < 1.5 Arcmin | ≤ 0.010 mm | Ø20mm - Ø160mm | ✓ Certified CE |
| RA-Heavy Fiber Tube | Zero-Backlash Strain Wave | 180 Nm | < 1.0 Arcmin | ≤ 0.008 mm | Ø20mm - Ø320mm | ✓ Certified CE |
| RA-Ultra Structural Pipe | Hydraulic / Direct Drive Servo | 650 Nm | < 0.5 Arcmin | ≤ 0.005 mm | Ø50mm - Ø500mm+ | ✓ Certified CE |
Built upon 35+ years of industrial CNC and laser machine design, our manufacturing infrastructure delivers unparalleled reliability, custom engineering, and global support.
Heavy-duty steel bed frames and rotary housings undergo high-temperature annealing and vibration stress relief to prevent mechanical deformation over decades of use.
In-house inventory of Yaskawa servo drives, CypCut control cards, replacement chuck jaws, bearings, and planetary gearboxes shipping globally same-day to minimize shop floor downtime.
Direct phone and video access to factory trained mechanical and application engineers—never automated ticket bots or call-centers. Dedicated pre-sale consultation and post-sale operator onboarding.
Every rotary attachment undergoes Renishaw laser interferometer dynamic calibration and load testing to guarantee angular accuracy before factory sign-off.
Detailed technical answers provided by our senior CNC application engineers to address common pre-purchase questions.
CE certification confirms that the rotary axis meets essential European health, safety, and environmental protection directives. Specifically, it certifies that electrical components satisfy the Low Voltage Directive (2014/35/EU), electromagnetic emissions do not interfere with external machinery under the EMC Directive (2014/30/EU), and mechanical pinch-points, dynamic braking, and structural safety factors comply with the Machinery Directive (2006/42/EC).
Choose a 3-jaw (or 4-jaw) chuck rotary axis when machining heavy pipes, metal tubes, or irregular profiles where positive physical clamping is required to resist cutting torque. Choose a roller-style rotary axis for delicate, thin-walled cylindrical objects (such as glass bottles, drinking tumblers, or thin acrylic tubes) that would crush or deform under mechanical jaw pressure.
Yes. If your current CNC software or controller supports a 4th axis output (e.g., CypCut, Syntec, Mach3, DSP, or Siemens Sinumerik), a rotary axis can be integrated using an auxiliary stepper or servo drive amplifier. Our engineering team provides custom wiring schematics, pinout diagrams, and controller configuration files to ensure rapid retrofit installation.
Gear backlash is minimized mechanically by utilizing zero-backlash harmonic strain wave gearboxes or precision helical planetary gearheads (rated under 1.5 arcminutes). In addition, controller software like CypCut or Syntec provides electronic backlash compensation values entered during laser interferometer calibration to adjust rotational acceleration steps in real time.
Our industrial rotary attachments feature IP65-rated sealed motor enclosures and double-lip oil seals around main drive spindles. This protects internal bearings, encoders, and gearboxes against metal chips, fine abrasive dust, ceramic particles, and direct liquid coolant spray during wet milling or high-pressure assist gas laser operations.
We specialize in OEM and ODM custom engineering. Our factory design team builds custom extended-bed tailstocks, pneumatic steady-rests for long flexible tubing, multi-jaw chuck adapters, and hollow-bore rotary spindles allowing continuous stock pass-through for long bar feed manufacturing.
Speak directly with our factory application engineers to select, configure, and specify the ideal CE-certified rotary axis attachment or multi-axis CNC machine for your production facility.
Inquire Now